Electrocoating (E-Coat)
How electrodeposition uses an electric current to build a uniform, self-limiting paint film on every wetted surface of a part — including recesses spray cannot reach.
Key takeaways
- Electrocoating immerses a conductive part in a waterborne paint bath and applies DC voltage, which drives charged paint particles onto the part.
- The deposited film is insulating, so deposition slows as the film builds — giving very uniform, self-limiting thickness.
- “Throwpower” lets e-coat reach inside box sections, seams and recesses that spray cannot coat.
- Cathodic epoxy e-coat is the standard corrosion primer for car bodies; cathodic acrylics are used where UV-stable single-coat finishes are needed.
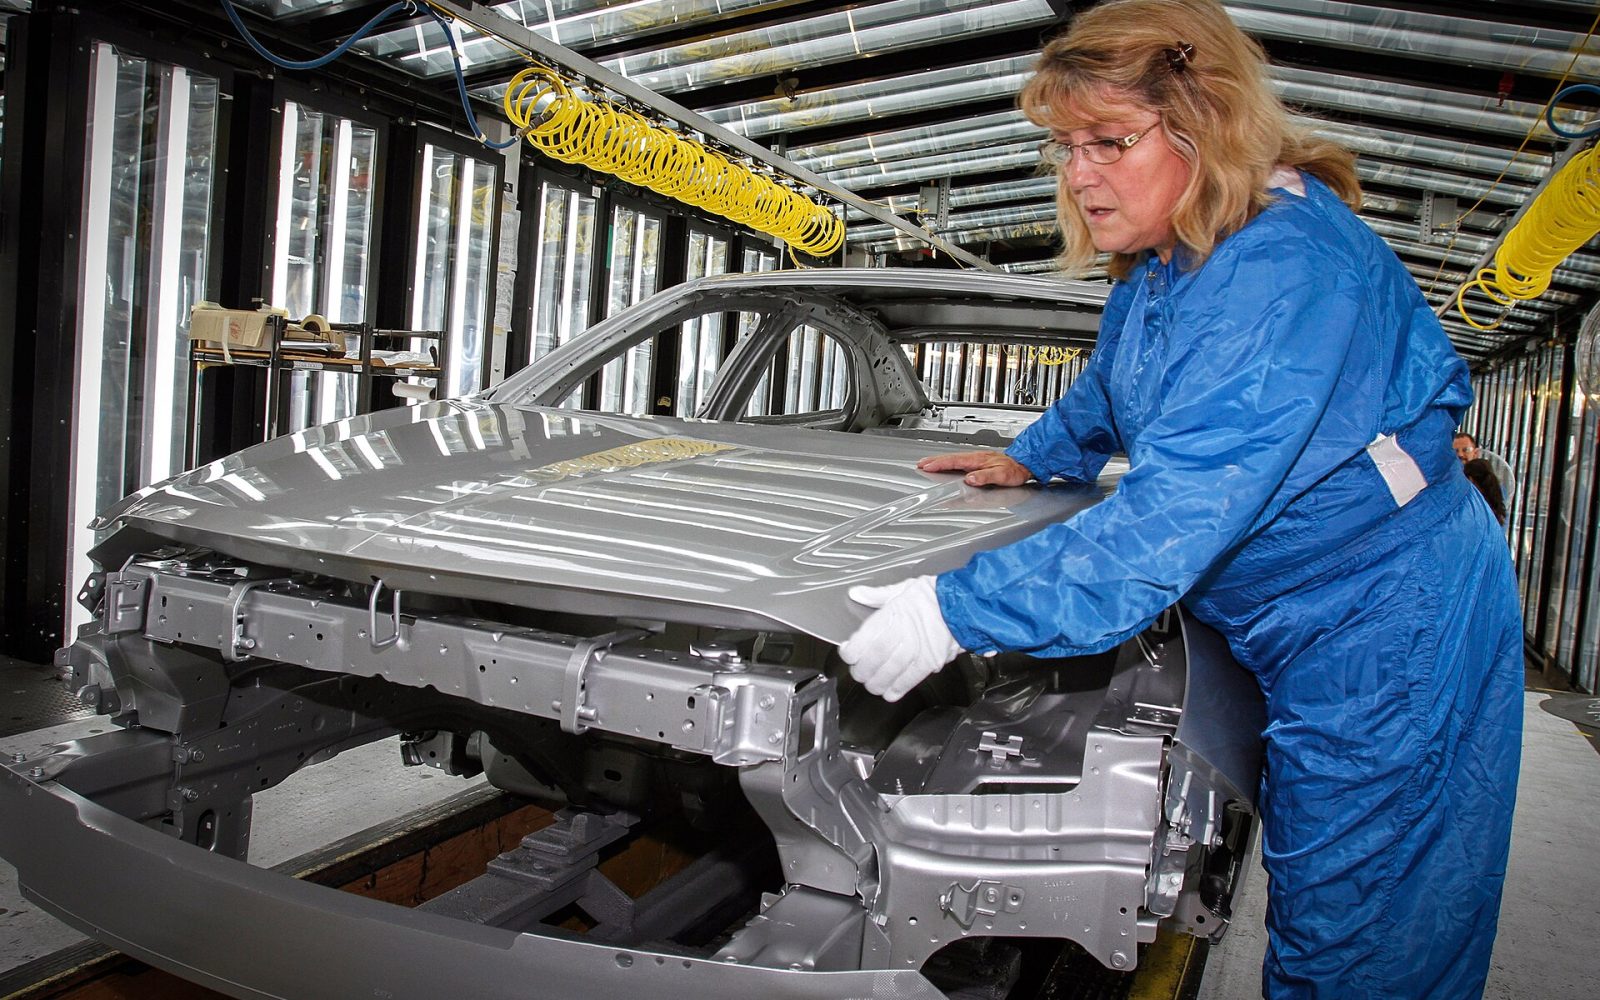
Electrocoating — also called e-coat, electrophoretic deposition or electropainting — is one of the most efficient and consistent ways to coat metal parts. It is used as the corrosion-protective primer on virtually all modern car bodies and on a wide range of other products, including truck and agricultural parts, appliances, fasteners, brackets, HVAC components and metal furniture.
Like dip coating, it immerses the part in a tank. The difference is that film formation is driven by electrochemistry rather than viscosity and drainage, which gives far better control over thickness and coverage.
How electrodeposition works
The e-coat bath is a dilute dispersion of resin and pigment in water, typically containing a modest percentage of solids. The resin particles carry an electrical charge. When the part (one electrode) and counter-electrodes in the tank are connected to a DC power supply, the charged particles migrate to the part. At its surface, electrochemical reactions change the local pH, destabilizing the particles so they coagulate into a film.
That film has high electrical resistance. As it grows, current through the coated areas falls, and deposition shifts to areas that are still bare or thinly coated. This is why e-coat builds to a near-uniform thickness and why it can reach into recesses: once exposed surfaces are insulated, current is driven deeper into the part. The ability to coat these recessed areas is called throwpower.
Cathodic vs anodic
| Feature | Cathodic (CED) | Anodic (AED) |
|---|---|---|
| Part polarity | Negative (cathode) | Positive (anode) |
| Typical resins | Epoxy, acrylic | Acrylic, polyester, epoxy |
| Corrosion resistance | Generally higher | Generally lower |
| Metal dissolution into film | Minimal | Some, as the part is the anode |
| Typical uses | Automotive bodies, parts, appliances | Lower-cost applications, some decorative uses |
Cathodic systems dominate today because the part is not oxidized during deposition and the films offer better corrosion resistance.
The e-coat process line
- Clean. Alkaline cleaning removes oils, drawing compounds and soils.
- Pretreat. A conversion coating — traditionally zinc phosphate, increasingly zirconium-based or similar thin-film pretreatments — improves adhesion and underfilm corrosion resistance.
- Rinse. Multiple rinses, ending in deionized water, keep contaminants out of the bath.
- Electrocoat. Parts enter the bath on conductive racks or carriers; voltage is applied, often with a controlled ramp, for a set time.
- Post-rinse. Loosely adhering “drag-out” paint is rinsed off with ultrafiltrate and returned to the bath.
- Bake. The film is cured in an oven to crosslink the resin; bake schedules are set by the coating supplier and commonly fall in the range of roughly 300–400 °F (about 150–200 °C).
The closed-loop rinse with ultrafiltration recovers paint that would otherwise be lost, which is a major reason e-coat can achieve very high material utilization, often cited as above 95%.
Controlling film build and bath health
Typical e-coat films are about 0.6–1.4 mils (15–35 µm), depending on the product and specification. Film build is controlled by:
- Voltage — higher voltage gives thicker films and better throwpower, up to the point of film rupture
- Immersion time under power
- Bath temperature — affects conductivity and deposition rate
- Bath solids, conductivity and pH — monitored daily and adjusted with replenishment
- Anode condition — counter-electrode cells and their anolyte circuits remove acid or base generated in the bath
Contamination from pretreatment chemicals, oils or poor rinsing causes craters, rough films and bath instability. Bath control is therefore as much a chemistry discipline as a coating one. Verify thickness on production parts with magnetic or eddy-current gauges (see dry film thickness measurement).
Pushing voltage too high to chase throwpower can cause rupture, where the film breaks down locally and leaves rough, porous spots. Stay within the supplier’s voltage window.
Advantages and limitations
Advantages
- Uniform, self-limiting film thickness
- Coats internal cavities, seams and edges well
- Very high material utilization with ultrafiltration
- Waterborne bath with low VOC content
- Highly automated and repeatable
Limitations
- Only conductive substrates can be coated
- High capital cost and large bath inventory
- Single color per tank; color changes impractical
- Film build limited; thick barrier coats need other methods
- Epoxy e-coats chalk under UV and need a topcoat outdoors
Applications and coating systems
In automotive OEM paint systems, cathodic epoxy e-coat forms the corrosion-protective base beneath primer-surfacer, basecoat and clearcoat. Because epoxy e-coat is not UV stable (see chalking and fading), exposed components either receive a topcoat — often powder or liquid — or use a UV-durable acrylic e-coat as a one-coat finish.
E-coat also serves as an excellent primer under other finishes on agricultural and construction equipment and general industrial parts, where its ability to coat every edge and recess limits edge corrosion and corrosion from inside box sections.
Design parts for e-coat: provide drain and vent holes so air can escape and bath can drain, avoid closed pockets that shield current, and plan rack contact points where small bare marks are acceptable.
Frequently asked questions
Can e-coat be applied to aluminum?
Yes. Aluminum, steel, galvanized steel and other conductive metals can be e-coated with appropriate pretreatment. Non-conductive plastics and composites cannot.
Why is e-coat usually black or gray?
Most e-coat is a primer, so color is not critical. Colored e-coats exist, but because each tank holds a single color, most lines run one standard primer color.
Does e-coat need a topcoat?
For exterior exposure, epoxy e-coat generally needs a UV-resistant topcoat. Acrylic e-coats can serve as a one-coat finish in many indoor or mild outdoor uses.
How thick can e-coat get?
Most products are designed for roughly 0.6–1.4 mils (15–35 µm). Some high-build formulations go thicker, but e-coat is not a heavy barrier coating.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.