Coating Quality Control Plans
What a coating quality control plan contains, how it differs from owner quality assurance, and how hold points, test frequencies and records turn a specification into verifiable work.
Key takeaways
- Quality control (QC) is the contractor’s own checking of its work; quality assurance (QA) is the owner’s verification that QC is working.
- A QC plan sets out who checks what, when, how and against which acceptance criteria — usually summarized in an inspection and test plan.
- Hold points stop work until a check is passed and recorded, which matters in coating because each step is covered by the next.
- Nonconformances need a defined route: identify, record, fix, re-inspect and close.
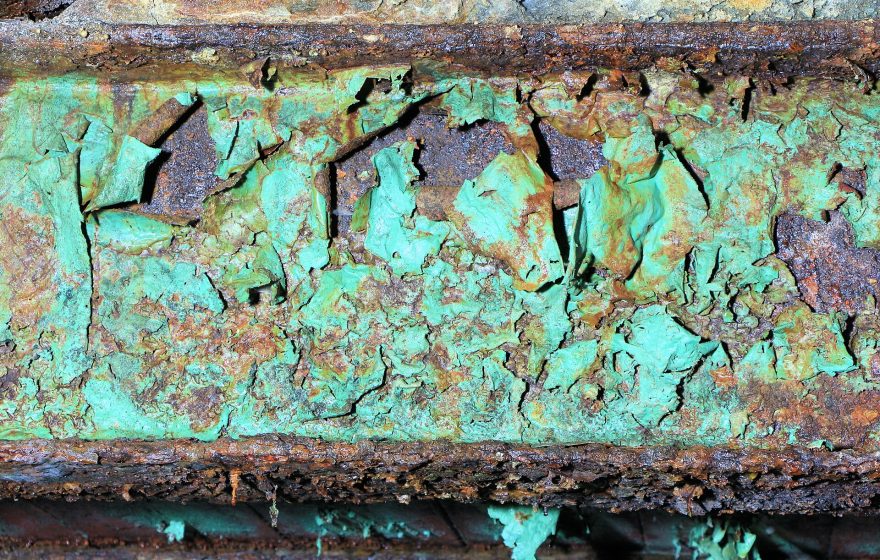
Coating work has an unforgiving property: once a coat is applied, the step beneath it can no longer be seen or easily tested. Poor surface preparation hidden under a perfect topcoat is still poor surface preparation. A quality control plan exists so that every critical step is checked and documented before it disappears.
Many specifications require a written QC plan as a submittal. Even when they do not, a plan protects the contractor — it is the evidence used when a warranty claim or dispute arises — and it is a core element of most contractor qualification programs.
Quality control versus quality assurance
The two terms are often used interchangeably, but on a coating project they describe different roles:
- Quality control is performed by the contractor’s own personnel — foreman, crew members or a dedicated QC inspector — to confirm the work meets the specification as it proceeds.
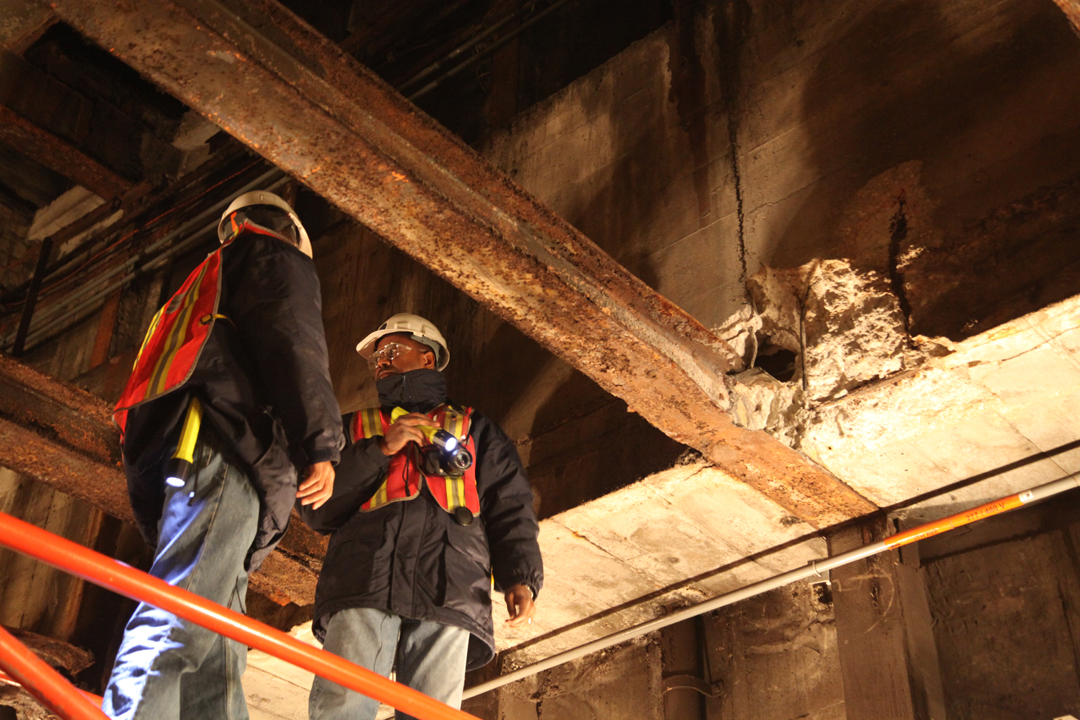
- Quality assurance is performed by or for the owner, often by a third-party inspector, to verify the contractor’s QC and spot-check results.
QA does not replace QC. An owner’s inspector who arrives once a day cannot see every blast cycle or every mixed kit; the contractor’s people can. A well-run job has both, with readings that broadly agree.
What a QC plan contains
- Scope and references. The project, the specification sections covered, and the standards and product data sheets that govern the work.
- Organization. Named QC personnel, their qualifications and their authority to stop work.
- Inspection and test plan. Each activity, the check, the method, the frequency, the acceptance criteria and whether it is a hold or witness point.
- Instruments. A list of gauges with calibration status and verification procedures.
- Records. Forms and daily inspection reports, how they are reviewed and where they are kept.
- Nonconformance and corrective action. How problems are recorded, resolved and prevented from recurring.
- Materials control. Receiving, batch tracking, storage temperature and shelf-life checks.
The inspection and test plan
The table shows typical entries for a blast-and-coat job on steel. Frequencies and acceptance criteria must come from the specification and product data sheets; the entries here are illustrative.
| Stage | Check | Typical method or reference | Control |
|---|---|---|---|
| Before preparation | Oil, grease, weld spatter, sharp edges | Visual; SSPC-SP 1 solvent cleaning where needed | Hold |
| Each shift and before coating | Air and surface temperature, relative humidity, dew point | Calibrated environmental instruments | Record; stop if out of limits |
| After blasting | Cleanliness grade | Specified SSPC/NACE or ISO 8501-1 grade with visual references | Hold |
| After blasting | Surface profile | ASTM D4417 — see profile measurement | Hold |
| After blasting | Soluble salts, dust | Method and limit per specification | Hold where specified |
| During application | Mixing, induction, pot life, wet film | Product data sheet; ASTM D4414 | Record |
| After each coat | Dry film thickness | SSPC-PA 2 / DFT measurement | Hold before next coat |
| Final | Continuity, appearance, cure | ASTM D5162 holiday testing where specified; visual | Hold for acceptance |
On concrete, entries change: moisture testing per ASTM F2170 or ASTM F1869, surface profile against ICRI 310.2R chips and, where specified, pull-off tests per ASTM D7234.
Hold points and witness points
A hold point is a stage where work must stop until the check is complete and, if specified, released by the owner’s inspector. A witness point gives the owner the option to attend, but work may proceed with notice. Agree which is which at the pre-job conference, along with how much notice inspectors need and what happens if they do not arrive.
Coating over a hold point that has not been released is one of the costliest mistakes on a job. Even if the work is sound, the contractor may be required to remove coating to prove it. Make releases explicit and recorded.
Handling nonconformances
- Identify and stop. Mark the affected area and halt work that would cover it.
- Record. Write a nonconformance report: location, requirement, actual result and readings.
- Determine disposition. Rework, repair, or — with owner approval only — accept as is.
- Correct. Carry out the repair using a defined procedure.
- Re-inspect and close. Re-test, record the result and close the report.
- Prevent recurrence. Identify the root cause — training, equipment, procedure — and address it.
Records and close-out
Good records are specific: location, time, instrument serial number, readings and the name of the person who took them. Photographs tied to locations add value. At close-out, compile the records into a turnover package with product batch numbers, data sheets, inspection reports, nonconformance logs and calibration certificates. That package becomes the baseline for future maintenance and any later investigation. A coating inspection checklist is a useful starting point for building forms.
Review QC records daily, not at the end of the job. A missing dew point reading discovered on the day can be explained; one discovered months later is simply a gap.
Frequently asked questions
Can the foreman also be the QC inspector?
On small jobs it is common, if the specification allows it. On larger or critical work, a dedicated QC person avoids the conflict between production and inspection.
How often should gauges be calibrated?
Follow the manufacturer’s recommendation and the specification, and verify accuracy on site with reference standards or shims before use, as SSPC-PA 2 describes for DFT gauges.
Is a QC plan required on every job?
Not always contractually, but every job benefits from a written plan scaled to its size. For small jobs, a one-page checklist with hold points may be enough.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.