Wet Film Thickness Measurement
How applicators use notch and wheel gauges to check wet film thickness as they work — and how to convert a wet reading into the dry film the specification requires.
Key takeaways
- Wet film thickness (WFT) is measured immediately after application so the applicator can correct film build while the coating is still workable.
- Target WFT is calculated from the specified dry film thickness (DFT) and the coating’s volume solids, adjusted for any thinner added.
- Notch (comb) gauges are cheap, quick and the most widely used; wheel gauges give finer resolution on smooth surfaces.
- WFT is a process control tool. Final acceptance is normally based on DFT measured after cure.
Most coating specifications state a required dry film thickness, but dry film can only be measured after the coating has cured — too late to fix a thin or heavy coat without extra work. Measuring wet film thickness while applying gives the applicator immediate feedback. Used consistently, it is the simplest way to hit the specified thickness, control material consumption and avoid defects caused by excessive build, such as sags and runs, mud cracking and solvent entrapment.
Calculating the target wet film
When a coating dries, the solvent or water evaporates and only the solids remain. The fraction of the wet volume that stays behind is the volume solids, listed on the product data sheet. The basic relationship is:
- WFT = DFT ÷ volume solids (volume solids as a decimal)
- With thinner added: WFT = DFT × (1 + thinner fraction) ÷ volume solids, where thinner fraction is the volume of thinner added per volume of coating
For example, for a target of 5 mils (127 µm) DFT with a coating of 70% volume solids, the target WFT is 5 ÷ 0.70 ≈ 7.1 mils (181 µm). If the coating is thinned 10% by volume, the target becomes 5 × 1.10 ÷ 0.70 ≈ 7.9 mils (200 µm). The site’s wet/dry film calculator can do the arithmetic.
| Target DFT | 50% volume solids | 70% volume solids | 100% solids |
|---|---|---|---|
| 2 mils (51 µm) | 4.0 mils (102 µm) | 2.9 mils (73 µm) | 2.0 mils (51 µm) |
| 4 mils (102 µm) | 8.0 mils (203 µm) | 5.7 mils (145 µm) | 4.0 mils (102 µm) |
| 6 mils (152 µm) | 12.0 mils (305 µm) | 8.6 mils (218 µm) | 6.0 mils (152 µm) |
| 10 mils (254 µm) | 20.0 mils (508 µm) | 14.3 mils (363 µm) | 10.0 mils (254 µm) |
Values assume no thinner. Read more on the underlying math in volume solids and coverage.
Types of wet film gauges
Notch (comb) gauges
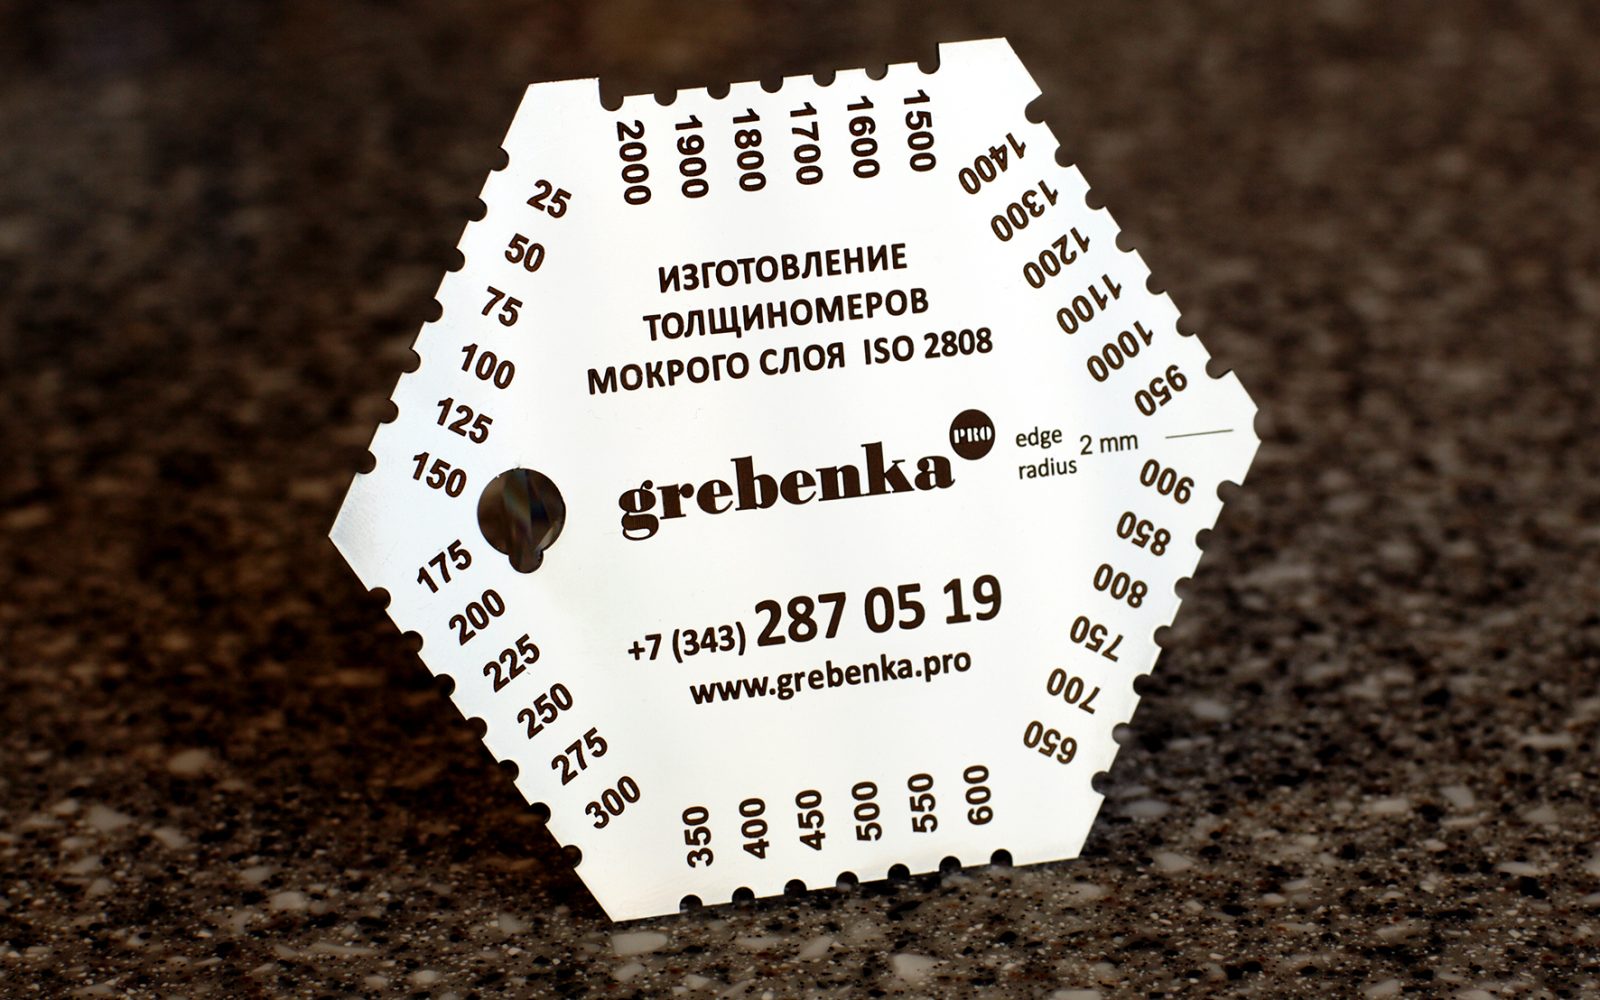
A notch gauge is a flat plate — square, hexagonal or comb-shaped — whose edges carry a series of teeth. The two outer teeth rest on the substrate, and the inner teeth are recessed by stepped amounts, each marked with its gap in mils or micrometers. ASTM D4414 describes measuring wet film thickness with notch gauges, and ISO 2808 includes comb gauges among its methods for determining film thickness.
Notch gauges are inexpensive, durable and quick, and are the standard tool on industrial and field work. Their resolution is limited to the step between teeth.
Wheel (eccentric roller) gauges
A wheel gauge has two outer rims of the same diameter and an eccentric center disc. Rolled through the wet film, the center disc first touches coating at a point that corresponds to film thickness, read from a scale on the rim. Wheel gauges offer finer resolution and are common in laboratory, product finishing and smooth-panel work, but they are less practical on rough or irregular field surfaces. ASTM D1212 also covers this style of gauge.
Wet film gauges are not calibrated in the way electronic DFT gauges are, but they do wear. Inspect teeth or rims for damage and replace gauges that are bent, nicked or coated with cured material.
How to take a reading with a notch gauge
- Measure immediately. Take the reading right after application, before solvent evaporates and the film shrinks.
- Press squarely. Place the gauge firmly and perpendicular to the surface so both end teeth touch the substrate.
- Withdraw and read. Lift the gauge straight off. Find the highest-numbered tooth that is wetted and the next tooth that is not. The film thickness lies between those two values; record the last wetted tooth value.
- Wipe clean. Clean the gauge with a compatible solvent before the next reading.
- Repeat and adjust. Take readings frequently across the work area and adjust technique, pass speed or tip size as needed.
On cylindrical surfaces such as pipe, orient the gauge along the length of the pipe so both end teeth sit on the surface. On curved surfaces in the other direction, readings can be misleading.
Gauge marks leave a small disturbed area in the wet film. Take readings where the mark can flow out or be brushed over — and on immersion linings, confirm whether gauge marks must be touched up before the coating sets.
Limitations and sources of error
- Fast-evaporating solvents. Coatings such as inorganic zinc and some lacquers lose solvent within seconds, so readings understate actual applied wet film.
- Surface profile. On blasted steel, the gauge teeth rest on profile peaks while some coating fills the valleys, so the reading may differ from the true average film. See surface profile measurement.
- Thixotropic and high-build coatings. Very thick, non-flowing films may not wet the teeth cleanly, making the reading ambiguous.
- Fast-set plural-component coatings. Polyureas and similar materials may gel before a reading can be taken; WFT is impractical and film build is controlled by technique and DFT checks.
- Porous substrates. Concrete and wood absorb some coating, so wet readings overstate what remains on the surface.
How WFT relates to DFT acceptance
Wet film readings are a guide, not an acceptance record. Most specifications accept the work based on DFT measured after cure, typically following SSPC-PA 2 or an equivalent sampling plan (see dry film thickness measurement). Inspectors may still record WFT checks in daily inspection reports to show the applicator was monitoring film build.
If WFT readings consistently meet the target but DFT comes in low, check the volume solids figure used, thinning practice, solvent loss and gauge technique before changing the application process.
Frequently asked questions
Can I use wet film readings instead of DFT measurements?
Not for acceptance in most specifications. WFT is a control tool during application; DFT after cure is the usual acceptance measurement.
Why is my calculated DFT higher than the measured DFT?
Common reasons include thinner not accounted for, solvent loss before measurement, coating absorbed into the substrate or profile, and inaccurate volume solids values.
Do I need a wet film gauge for 100% solids coatings?
Yes, if the material stays liquid long enough to measure. With no solvent, WFT and DFT are essentially equal, which makes checks simple.
How often should I take wet film readings?
Frequently enough to catch drift — commonly every few square meters or each pass on critical work. The quality control plan may set a minimum frequency.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.