Fire & Explosion Hazards in Coating Work
Why solvent vapors, spray mist and coating dust can ignite, how flash point and explosive limits work, and the ventilation, grounding and ignition controls that prevent fires and explosions.
Key takeaways
- Most solvent-borne coatings, thinners and cleaners are flammable liquids; their vapors can ignite well below the temperatures people associate with fire.
- A vapor–air mixture can only ignite between its lower and upper explosive limits (LEL and UEL); ventilation aims to keep concentrations far below the LEL.
- Static electricity from spraying, pumping and pouring is a common, invisible ignition source — bond and ground equipment and containers.
- Enclosed spaces, spray booths, solvent storage, powder coating and oily rags each need specific controls; follow the SDS, fire codes and your employer’s program.
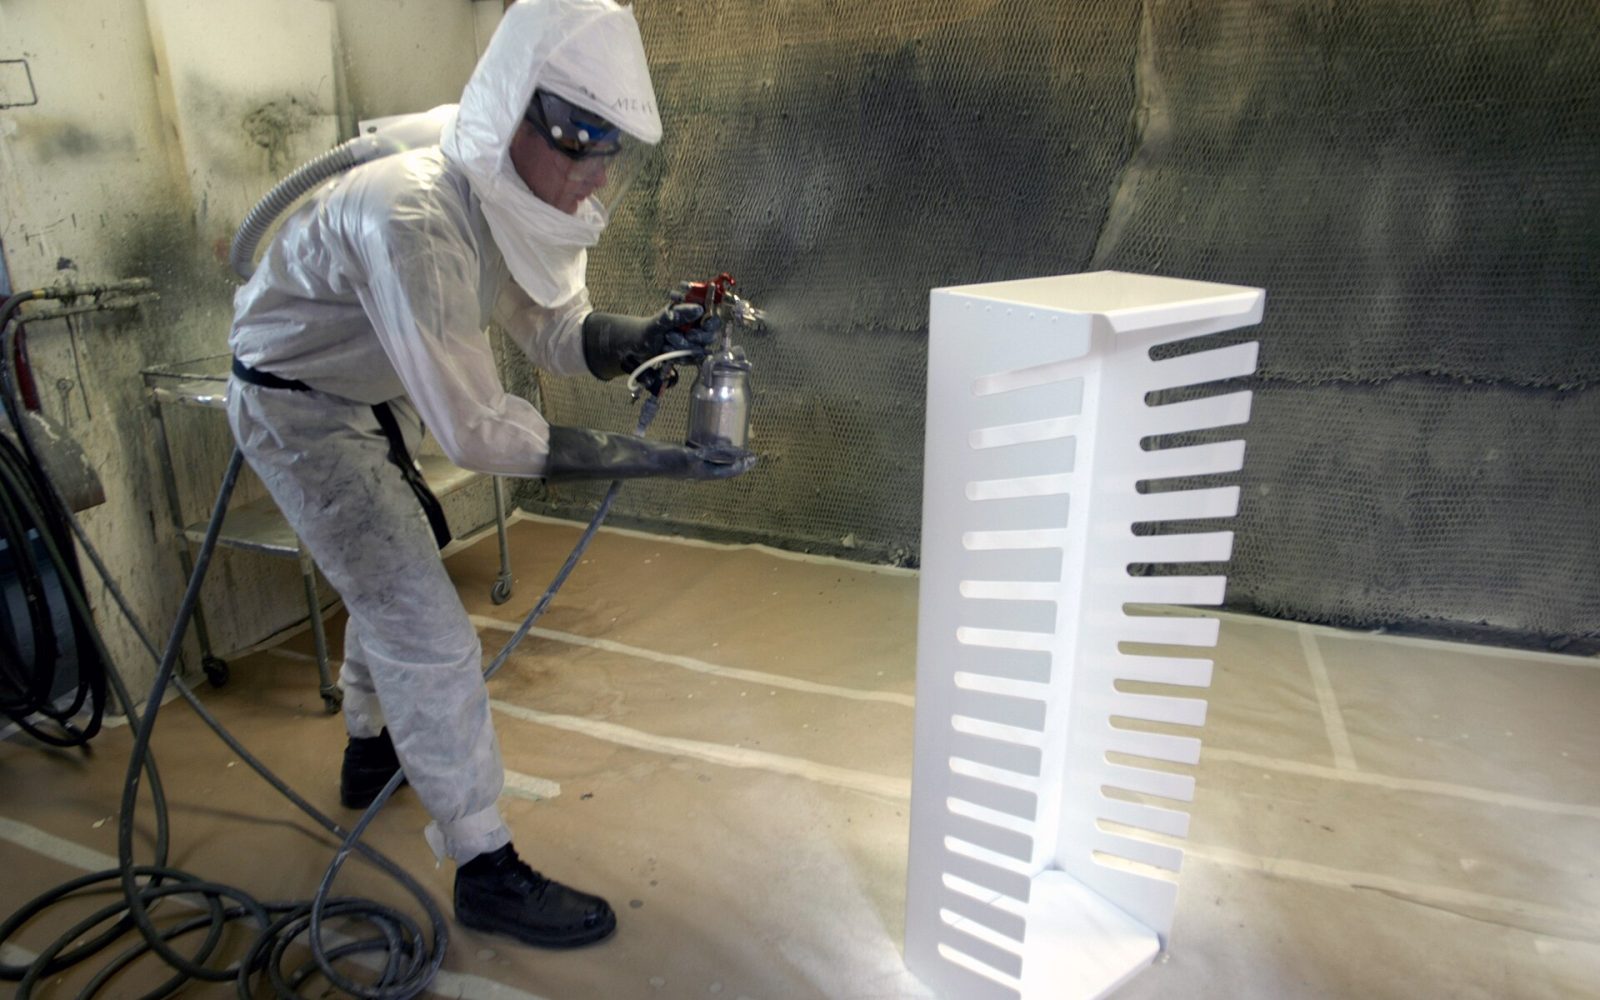
Coating work routinely brings together the three sides of the fire triangle: fuel (solvent vapor, spray mist or powder), oxygen (air) and ignition sources (sparks, static, hot surfaces, flames). In an open area the result is usually a fire. In an enclosed space — a tank, hull, booth or containment — the same conditions can produce an explosion or flash fire that injures or kills workers before they can react.
This article explains the key concepts and controls. It does not replace fire codes, the product SDS, your employer’s hot-work and fire-prevention programs, or local regulations.
Flash point and explosive limits
Three properties, all found in Section 9 of the safety data sheet, describe how easily a coating or solvent will burn:
- Flash point — the lowest liquid temperature at which enough vapor forms to ignite momentarily in air near the surface. A product with a flash point below the ambient or surface temperature is giving off ignitable vapor as you work. Fast solvents such as acetone and methyl ethyl ketone have flash points well below normal room temperature.
- Lower explosive limit (LEL or LFL) — the minimum vapor concentration in air that can ignite. For common coating solvents it is typically in the range of roughly 1–3% by volume — still an enormous concentration in exposure terms.
- Upper explosive limit (UEL or UFL) — the concentration above which the mixture is too rich to burn. A “too rich” atmosphere is still dangerous, because it passes back through the explosive range as it is diluted.
Most solvent vapors are heavier than air. They flow downhill, collect in sumps, pits, tank bottoms and the lower parts of hulls, and can travel to a distant ignition source and flash back. Consult solvents in coatings for how solvent blends are formulated.
Flammability categories
Under the Globally Harmonized System (GHS), adopted in OSHA’s Hazard Communication Standard and in many other countries, flammable liquids are classified by flash point and boiling point:
| GHS category | Criteria | Signal word |
|---|---|---|
| Category 1 | Flash point < 23 °C (73.4 °F) and initial boiling point ≤ 35 °C (95 °F) | Danger |
| Category 2 | Flash point < 23 °C (73.4 °F) and initial boiling point > 35 °C (95 °F) | Danger |
| Category 3 | Flash point ≥ 23 °C and ≤ 60 °C (73.4–140 °F) | Warning |
| Category 4 | Flash point > 60 °C and ≤ 93 °C (140–199.4 °F) | Warning |
Many solvent-borne industrial coatings and thinners fall into Categories 2 or 3. Waterborne and 100%-solids products usually have higher flash points, but “low-VOC” does not automatically mean nonflammable — check the SDS, and remember the thinner and cleanup solvent may be far more flammable than the coating.
Ignition sources
Static electricity
Fluid moving at high pressure through hoses, guns and tips generates static charge, as does pouring, pumping and even wiping with synthetic cloths. Airless spray and plural-component equipment should be grounded according to the manufacturer’s instructions, conductive hoses used where specified, and metal containers bonded to each other and grounded when transferring liquids. Spray into a grounded metal pail when flushing, and keep the gun in firm contact with the pail. NFPA 77 provides guidance on static electricity hazards.
Electrical equipment and lighting
Where flammable vapors may be present, lights, fans, heaters and tools must be suitable for the hazardous location — typically explosion-proof or intrinsically safe equipment rated for the area classification. Ordinary extension cords, work lights and phones can be ignition sources.
Hot work, heaters and other sources
Welding, cutting and grinding sparks can travel a long way and ignite vapor or residues. Hot work near coating operations should be controlled through a permit system; NFPA 51B covers fire prevention during hot work. Direct-fired heaters, engines, smoking, friction sparks and hot surfaces are other common sources.
Enclosed spaces, booths and storage
- Confined and enclosed spaces. Ventilation and continuous monitoring with a calibrated combustible-gas meter are essential. Many programs halt work or prohibit entry above 10% of the LEL, consistent with the hazardous-atmosphere definition in OSHA’s permit-required confined space rule (29 CFR 1910.146). See confined space coating work and ventilation for coating work.
- Spray booths and finishing rooms. NFPA 33 and OSHA’s spray finishing rule (29 CFR 1910.107) address booth construction, ventilation, electrical classification, fire protection and residue control. Overspray deposits on filters and booth surfaces are fuel and must be cleaned regularly.
- Storage. Keep flammable liquids in closed, labeled containers, in approved cabinets or rooms, limiting quantities at the work area as NFPA 30 and local fire codes require.
- Powder coating. Finely divided powder coatings are combustible dusts. Booth airflow, grounding of parts and equipment, and housekeeping keep dust clouds below explosive concentrations.
Rags soaked with drying oils or oil-based stains and coatings — linseed oil, alkyds and similar products — can heat up and ignite on their own as they oxidize. Spread them flat to dry outdoors away from buildings, or store them in a closed metal container filled with water, then dispose of them according to local rules.
A fire-prevention checklist
- Review the SDS. Note flash points and flammability categories for coatings, thinners and cleaners.
- Control vapors. Ventilate to keep concentrations well below the LEL and confirm with monitoring.
- Remove ignition sources. Use rated electrical equipment, issue hot-work permits, post no-smoking signs and isolate heaters.
- Bond and ground. Ground pumps, guns, containers and conductive work pieces before spraying or transferring liquids.
- Limit fuel. Keep only the quantity needed at the work area, keep lids closed and manage waste rags safely.
- Prepare for emergencies. Provide suitable extinguishers, clear escape routes, a fire watch where required and a rescue plan for enclosed spaces.
Ventilation calculated only to stay below the LEL is rarely enough to protect health. Occupational exposure limits for solvents are typically far lower than 10% of the LEL, so design airflow for both — and use respirators where exposure limits may still be exceeded.
Frequently asked questions
Can waterborne coatings catch fire?
Liquid waterborne coatings are usually much less flammable than solvent-borne ones, but some contain flammable co-solvents, and dried films and overspray residues can burn. Check the SDS flash point and flammability classification.
What does “explosion-proof” mean?
Explosion-proof equipment is built to contain an internal ignition and prevent it from igniting the surrounding atmosphere. It must be rated for the specific hazardous location classification and maintained in its rated condition.
Is a combustible-gas meter reading of zero proof that a space is safe?
Not by itself. Meters must be calibrated and bump-tested, readings should be taken at several heights because vapors stratify, and toxic exposure and oxygen levels must also be checked.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.