Flash Rust
Flash rust is the thin, fast-forming oxide that appears on freshly cleaned steel as it dries after waterjetting or wet blasting. How much a coating can tolerate depends on the grade and the product.
Key takeaways
- Flash rust is a thin layer of rust that forms on bare, freshly cleaned steel as it dries after contact with water, typically within minutes to a few hours.
- It is graded Light, Medium or Heavy using visual references such as ISO 8501-4 and SSPC-VIS 4/NACE VIS 7 (waterjetting) or SSPC-VIS 5/NACE VIS 9 (wet abrasive blasting).
- Many surface-tolerant coatings accept light flash rust; heavy flash rust, loose rust and rust on salt-contaminated steel generally must be removed.
- Low-salt rinse water, fast drying, controlled humidity and coating promptly are the best defences.
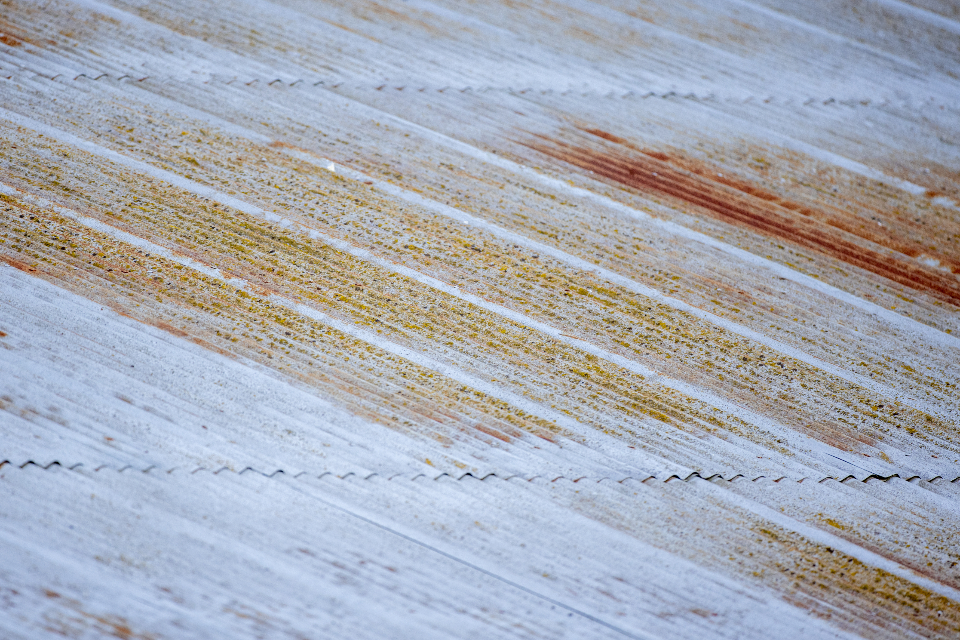
Anyone who has used waterjetting or wet abrasive blasting knows the moment: a bright, freshly cleaned steel surface turns golden-brown as it dries. That discoloration is flash rust. It is not a sign the cleaning failed, but it must be understood, graded and controlled before coating.
Flash rust is specific to wet methods. Rust that develops on dry-blasted steel left too long before coating is usually called rust-back or rust bloom; it has similar causes but is assessed against the original dry blast standard rather than a flash rust grade.
Why flash rust forms
Corrosion needs an anode, a cathode, an electrolyte and a conductive path (see corrosion science basics). Freshly cleaned steel is chemically very active, and a film of water supplies the electrolyte. As the film thins during drying, oxygen reaches the steel easily and a thin oxide forms quickly across the surface.
Several factors control how fast and how heavily it forms:
- Drying time. The longer the steel stays wet, the heavier the rust. Shaded, cold or poorly ventilated areas rust more than surfaces in sun and moving air.
- Humidity and temperature. High relative humidity and steel close to the dew point slow drying and favor oxidation.
- Soluble salts. Chlorides and sulfates, whether left on the steel or present in the water, make the film far more conductive and drive heavier, faster rusting (see soluble salt contamination).
- Water quality. Water with dissolved salts or iron contributes contamination of its own.
- Surface condition. Pitted steel holds water in pits, which tend to rust first and heaviest.
Flash rust grades
Two visual reference families are widely used. ISO 8501-4 covers surfaces prepared by high-pressure waterjetting and defines flash rust grades. SSPC-VIS 4/NACE VIS 7 provides photographs for waterjetted surfaces, and SSPC-VIS 5/NACE VIS 9 does the same for wet abrasive blasting, each including flash rust levels. The wording varies between documents, but the grades follow the same logic:
| Grade | Appearance | Typical wipe/tape result | Common treatment |
|---|---|---|---|
| Light (L) | Thin, yellow-brown discoloration; original steel surface still visible | Little or no transfer to a cloth | Often acceptable for coatings rated for it |
| Medium (M) | Layer of rust that obscures the original steel | Noticeable marking of a cloth | Acceptable only if the specification and PDS allow |
| Heavy (H) | Thick, red-brown, loosely adherent rust | Readily marks a cloth; may come off in flakes | Remove and re-clean before coating |
Grades are judged visually and, often, by wiping the surface with a clean cloth or applying adhesive tape and looking at the transfer. The project specification should state the maximum flash rust grade allowed at the time of coating.
How much flash rust can coatings tolerate?
Tolerance depends on the coating chemistry and the service. Surface-tolerant products such as many epoxy mastics are formulated to wet and penetrate light oxides. Some waterborne and moisture-tolerant primers are designed specifically for wet-prepared steel. On the other hand, inorganic zinc primers, thin-film linings and coatings for immersion or high-temperature service commonly demand little or no flash rust.
Light flash rust is a thin, adherent oxide. Heavier rust is loosely bound, so coating it builds on a weak layer that can fail by delamination. The product data sheet is the deciding document: it should state whether flash rust is acceptable and to what grade.
Flash rust that reappears quickly and heavily, especially in spots or streaks, is often a symptom of soluble salts rather than just slow drying. Test for chlorides before simply re-cleaning; otherwise the rust will come back, under the coating as well as on top of the steel.
Preventing and controlling flash rust
- Use clean water. Use potable or low-conductivity water for jetting and rinsing so the process removes salts rather than adding them.
- Dry fast. Blow down with clean, dry compressed air, ventilate, and, where needed, use heaters or dehumidifiers (see dehumidification and climate control).
- Control humidity. Keep the steel temperature above the dew point by the specified margin, commonly at least 5 °F (3 °C).
- Work in sections. Clean only the area that can be dried, inspected and coated within the same shift.
- Consider inhibitors carefully. Flash rust inhibitors added to the water can delay rusting, but some leave residues that interfere with adhesion. Use only inhibitors approved by the coating manufacturer.
- Coat promptly. Apply the primer as soon as the surface meets the specified dryness, cleanliness and flash rust grade.
Removing excessive flash rust
If flash rust exceeds the specified grade, it must be removed before coating. Options include:
- Re-waterjetting the area and drying it faster the second time.
- A light dry abrasive sweep blast, where dry blasting is allowed.
- Power-tool or hand-tool cleaning for small areas, if the specification permits and the result still meets the required standard.
Do not wire-brush heavy flash rust and coat over the remaining film. Burnishing loose rust creates a polished, poorly bonded layer, and any salts under it remain in place.
Frequently asked questions
Is flash rust bad for coatings?
Light flash rust is acceptable for many coatings designed for wet-prepared steel. Medium and heavy flash rust reduce adhesion and should be removed unless the product data sheet and specification explicitly allow them.
How fast does flash rust form?
Often within minutes to a few hours of the steel getting wet, depending on humidity, temperature, airflow and salt contamination.
Is flash rust the same as rust-back?
They are related but not identical. Flash rust forms during drying after wet cleaning; rust-back forms on dry-blasted steel left uncoated in humid conditions. Both indicate the surface no longer meets its original condition.
Do flash rust inhibitors cause problems?
They can. Some leave residues that affect adhesion or contribute to osmotic blistering. Use only inhibitors the coating manufacturer has approved, at the stated concentration.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.