Pipeline Coatings
The external coatings — FBE, 3LPE, 3LPP and field joint systems — that work with cathodic protection to keep buried and subsea pipelines intact for decades.
Key takeaways
- Buried and submerged steel pipelines are protected by an external coating working together with cathodic protection (CP); the coating does most of the work and CP protects the defects.
- Fusion-bonded epoxy (FBE) and three-layer polyolefin systems (3LPE and 3LPP) dominate modern plant-applied external coatings.
- Girth welds are coated in the field with heat-shrink sleeves, liquid epoxies or polyurethanes, or induction-applied FBE — often the weakest link.
- Good pipeline coatings resist cathodic disbondment and, if they do fail, should not shield CP current from the steel.
- Holiday detection during construction and above-ground surveys during operation verify coating integrity.
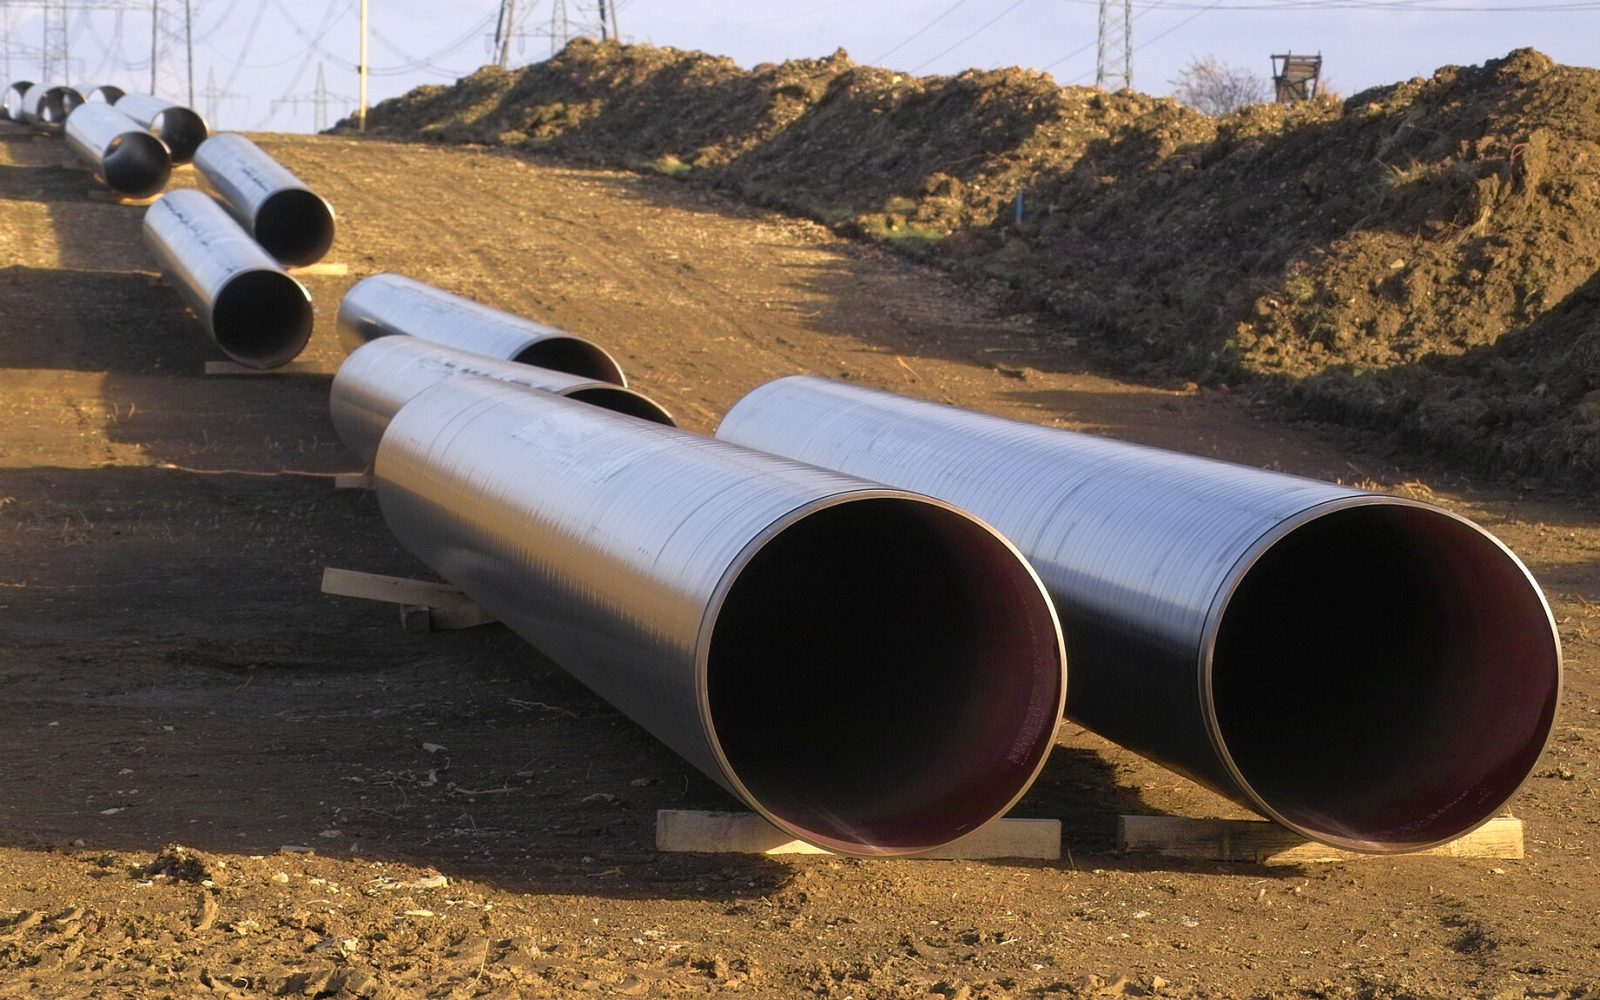
Pipelines carrying oil, gas, water and other products run for thousands of kilometres through soils, river crossings, swamps and seabeds, where steel would quickly corrode without protection. The external coating is the primary barrier, and in most jurisdictions buried steel transmission pipelines must be both coated and cathodically protected — in the United States, for example, under the federal pipeline safety regulations at 49 CFR Parts 192 (gas) and 195 (hazardous liquids).
Pipeline coatings face demands that few other coatings do: handling, bending and transport at the coating plant, backfill and rock impact, soil stresses, elevated operating temperatures and decades of service with almost no opportunity for inspection or repair.
How coatings and cathodic protection work together
No coating is perfect over hundreds of kilometres; holidays and damage are inevitable. Cathodic protection — via sacrificial anodes or impressed current — shifts the potential of exposed steel so it does not corrode. A good coating reduces the bare area so the CP current requirement stays manageable. The fundamentals are covered in corrosion science basics.
Two coating properties matter specifically in CP service:
- Cathodic disbondment resistance — at holidays, CP generates alkaline conditions that can progressively undermine coating adhesion. Coatings are qualified with cathodic disbondment tests specified in standards such as ISO 21809 and CSA Z245.20, and in ASTM methods such as ASTM G8 and G42.
- Not shielding CP — if a high-resistance coating disbonds but remains intact as a tent over the steel, it can block CP current from reaching water trapped underneath, allowing corrosion and contributing to stress corrosion cracking risk. Disbonded polyolefin tapes and some older systems are known for this; FBE tends to fail in a way that still allows CP current through.
Main external coating systems
| System | Construction | Typical thickness | Notes |
|---|---|---|---|
| Fusion-bonded epoxy (FBE) | Single layer of thermoset epoxy powder | Commonly ~350–500 µm (14–20 mils) | Excellent adhesion and CD resistance; does not shield CP; susceptible to impact damage |
| Dual-layer FBE | FBE base plus tougher FBE abrasion-resistant overcoat | Total often ~750–1,000+ µm (30–40+ mils) | Used for directional drilling, boring and rocky terrain |
| Three-layer polyethylene (3LPE) | FBE primer, copolymer adhesive, extruded polyethylene | Total commonly ~2–4 mm (80–160 mils) | Excellent mechanical protection and low water uptake; commonly rated to roughly 80–85 °C (176–185 °F) |
| Three-layer polypropylene (3LPP) | FBE primer, adhesive, extruded polypropylene | Total commonly ~2–5 mm | Higher operating temperatures than 3LPE, commonly above 100 °C (212 °F); common offshore |
| Coal tar and asphalt enamels, tapes | Legacy hot-applied enamels and wrapped tapes | Varies | Found on older lines; enamels largely replaced for health and environmental reasons |
| Concrete weight coating | Reinforced concrete over the anticorrosion coating | Tens of millimetres | Provides negative buoyancy and mechanical protection offshore and at crossings |
Thickness and temperature figures are indicative; actual limits depend on the specific materials, pipe diameter and project specification. The main international product standards are the ISO 21809 series (external coatings for buried or submerged pipelines), with parts covering polyolefin coatings, FBE, field joint coatings and concrete weight coatings, and in Canada the CSA Z245.20 (plant-applied external coatings such as FBE) and CSA Z245.21 (plant-applied polyethylene) standards.
How FBE is applied
In a coating plant, pipe is cleaned, abrasive blasted to near-white metal with an angular profile, often given a chemical pretreatment, then induction-heated — commonly to roughly 200–250 °C (390–480 °F), as the powder supplier specifies. Epoxy powder is sprayed electrostatically onto the hot pipe, where it melts, flows and cures within seconds to minutes before water quenching. See electrostatic application and epoxy coatings. For 3LPE and 3LPP, the adhesive and polyolefin layers are extruded over the FBE while it is still reactive.
Internal coatings serve different purposes. In gas transmission lines, thin internal epoxy “flow coats” reduce friction and keep pipe clean during storage (API RP 5L2 covers this service), while water, oil and produced-water lines may use thicker internal linings for corrosion protection.
Field joints, bends and repairs
Pipe is coated in the plant with bare cutbacks at each end so it can be welded in the field. Every girth weld must then be coated on site, often in poor weather and against a tight construction schedule. Common field joint coatings include:
- Heat-shrinkable sleeves — cross-linked polyolefin backings with adhesive, shrunk over the preheated joint.
- Liquid epoxy and polyurethane — high-build, 100% solids coatings applied by brush, roller or spray; widely used and compatible with FBE line pipe.
- Induction-applied FBE — FBE powder applied to the induction-heated joint, matching the line coating.
- Injection-molded polypropylene and similar — used offshore with 3LPP line pipe.
- Viscoelastic and tape systems — used particularly for repair and rehabilitation.
- Clean. Remove oil, grease and weld debris; check that factory coating chamfers are sound.
- Blast. Abrasive blast the joint, typically to Sa 2½ (SSPC-SP 10/NACE No. 2) or as specified, with a profile commonly in the ~50–100 µm (2–4 mil) range. See abrasive blasting.
- Preheat. Heat the steel to the specified temperature, which also drives off moisture and keeps the surface above the dew point.
- Apply. Apply the joint coating with the specified overlap onto the factory coating.
- Inspect. Check thickness, adhesion and appearance; holiday-test before lowering in.
Inspection and integrity
Coating integrity is checked at several stages. In the plant, coatings are tested for thickness, adhesion, cure, impact resistance and cathodic disbondment per the product standard. During construction, the entire pipe is passed through a holiday detector immediately before lowering into the trench; NACE SP0490 covers holiday detection of FBE coatings of 250–760 µm (10–30 mils), and NACE SP0274 covers high-voltage electrical inspection of pipeline coatings more generally. Test voltage is set from coating type and thickness to find defects without damaging sound coating. See holiday testing.
After burial, operators monitor CP and use above-ground surveys such as direct current voltage gradient (DCVG) and alternating current voltage gradient (ACVG) to locate coating defects, followed by excavation and direct assessment where needed.
Rocky backfill, careless handling and pipe skids damage coatings. Padding, rock shield, appropriate backfill and careful pipe handling are as important to coating integrity as the material itself.
Rehabilitation of existing pipelines
When older coatings such as tapes or enamels disbond or degrade, sections are excavated, the old coating removed, the steel blast-cleaned and assessed for corrosion and cracking, and the pipe recoated — commonly with high-build liquid epoxies or polyurethanes designed for field application. Coating selection considers operating temperature, soil stress, compatibility with adjacent coatings and CP, and the conditions of in-ditch application.
Frequently asked questions
Why is FBE so widely used?
FBE bonds very strongly to blasted steel, resists cathodic disbondment well, tolerates a range of soils and does not shield CP current if it fails. It is also a fast, efficient plant process.
When is 3LPE preferred over FBE?
Three-layer polyolefins offer much greater mechanical protection and lower moisture permeation, which suits rocky terrain, large-diameter lines and long-distance transport and handling. FBE is often favored where its thinner film, lower cost and CP behavior are advantageous.
Can a coating replace cathodic protection?
No. Coatings always contain some defects and are damaged during construction and service. Regulations and good practice require CP alongside coating for buried and submerged steel pipelines.
What limits pipeline coating temperature?
Each coating has an operating temperature rating tied to its glass transition temperature or softening behavior; exceeding it accelerates disbondment and degradation. Hot lines require high-temperature FBE, 3LPP or other specialized systems.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.