Pharmaceutical & Cleanroom Coatings
Seamless, low-shedding floor and wall systems for pharmaceutical plants, laboratories, hospitals and electronics cleanrooms — built to survive aggressive disinfectants and strict audits.
Key takeaways
- Pharmaceutical and cleanroom surfaces must be smooth, impervious, seamless and cleanable, and must not shed particles into the controlled environment.
- Repeated exposure to disinfectants and sporicides — hydrogen peroxide, peracetic acid, sodium hypochlorite, alcohols and quaternary ammonium compounds — is often the most demanding chemical exposure.
- Electronics cleanrooms and solvent-handling areas often need static-control flooring tested to recognized ESD methods.
- Coatings work in a regulated facility is a change that must be planned with quality assurance, documented and followed by cleaning and requalification.
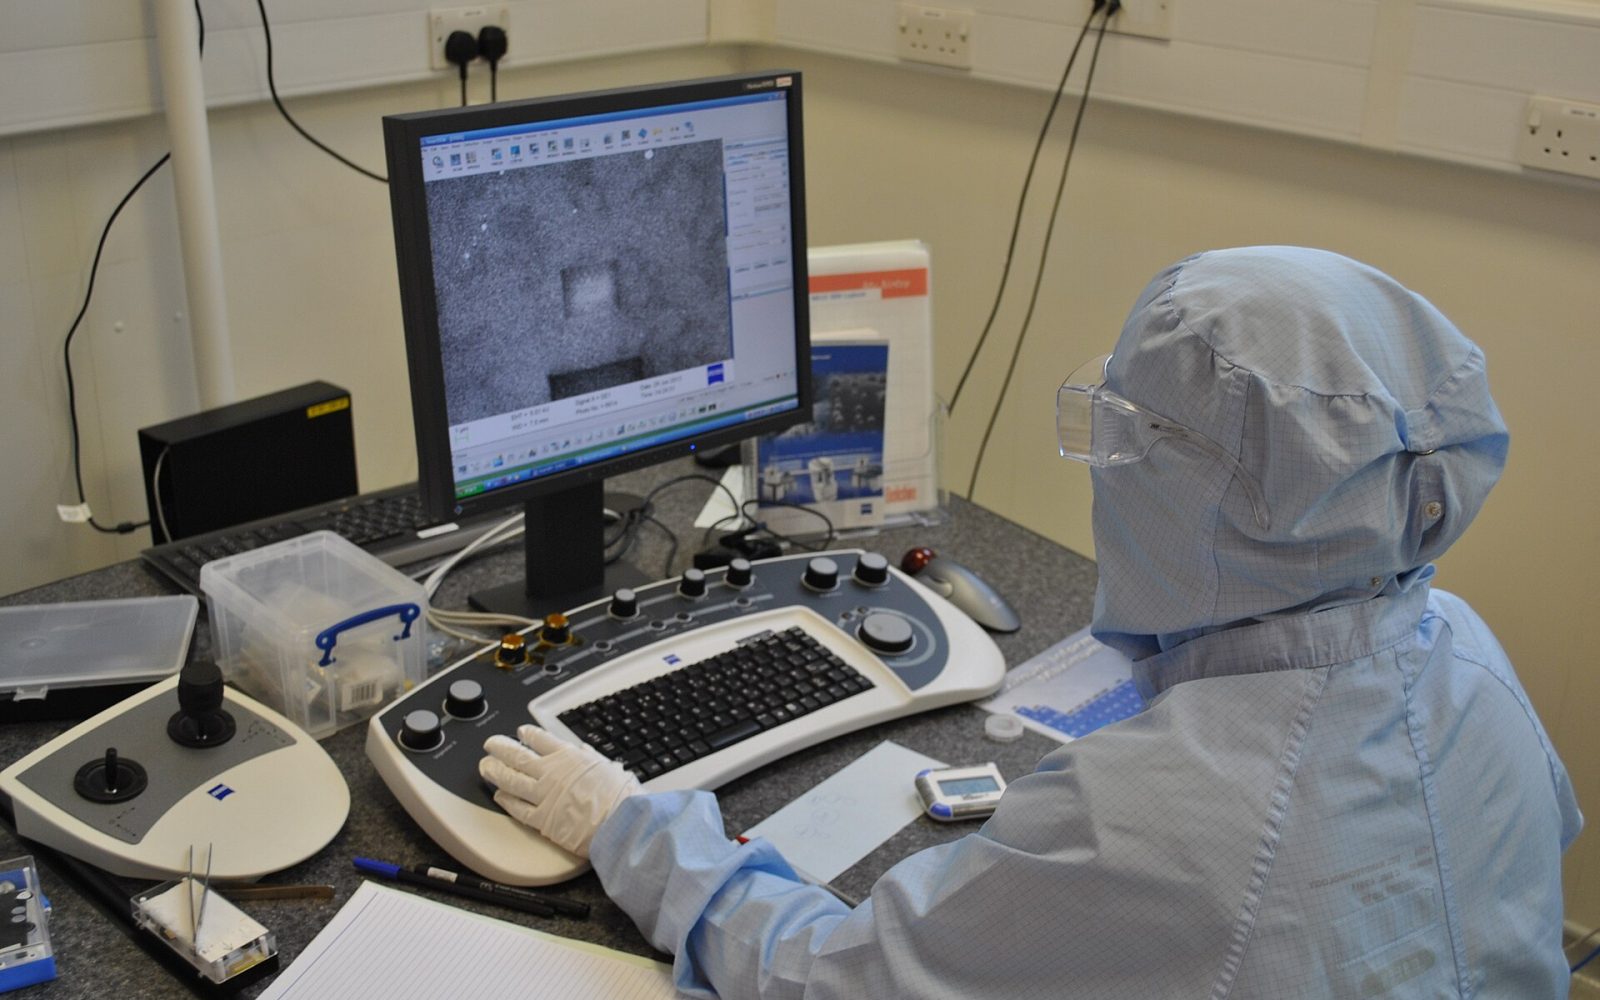
Pharmaceutical and cleanroom coatings cover the floors, walls, ceilings and some equipment surfaces in drug manufacturing plants, biotechnology suites, compounding pharmacies, hospital operating and isolation rooms, laboratories, and semiconductor and electronics cleanrooms. These environments control airborne particles, microorganisms and sometimes electrostatic charge. Surfaces must support those controls: a coating that chalks, cracks, absorbs disinfectant or leaves crevices around a pipe penetration can become a contamination source and an audit finding.
Regulatory and design context
Coating selection follows from facility requirements rather than from any single coating standard:
- Good Manufacturing Practice (GMP). In the United States, current GMP regulations for finished pharmaceuticals (21 CFR Part 211) require buildings with surfaces suitable for cleaning and maintenance. In Europe, EU GMP Annex 1 on sterile manufacturing calls for smooth, impervious, unbroken surfaces in clean areas that minimize shedding and accumulation of particles and withstand repeated cleaning and disinfection.
- ISO 14644-1 classifies cleanrooms by airborne particle concentration, from very stringent classes used in semiconductor work to less stringent classes used for supporting areas.
- Static control programs in electronics manufacturing commonly follow ANSI/ESD S20.20, with floor resistance measured by methods such as ASTM F150.
Owners usually translate these into a user requirement specification for finishes, which the coating system must meet and which validation teams later verify.
What cleanroom surfaces must do
| Requirement | Why it matters | How coatings achieve it |
|---|---|---|
| Seamless, non-porous surface | No crevices for microbes or particles | Monolithic resin floors and walls with integral coves |
| Disinfectant resistance | Daily cleaning plus periodic sporicide use | Highly crosslinked epoxy, polyurethane or vinyl ester chemistries |
| Low particle shedding | Airborne particle limits for the room class | Hard, non-chalking, abrasion-resistant finishes |
| Low outgassing | Airborne molecular contamination in sensitive processes | Fully cured, low-VOC or solvent-free systems |
| Static control (where required) | Protects electronics and reduces ignition risk | Conductive or static-dissipative floor systems |
| Cleanability and color | Visual confirmation of cleanliness | Smooth or lightly textured, usually light colors |
Floor systems
Common options include self-leveling epoxy and polyurethane floors, typically around 1/16–⅛ in (1.5–3 mm), for clean production areas; urethane cement in wet processing, wash and utility areas; and MMA where shutdown time is very short and odor can be managed. Seamless resin floors with coves are generally preferred over sheet vinyl with welded seams in the most critical areas, though sheet goods remain common in hospitals and laboratories.
Slip resistance must be balanced with cleanability: cleanroom floors are usually smooth or very finely textured, while wash rooms and wet corridors may need more grip. For floor chemistries, see epoxy coatings, urethane cement flooring and concrete floor coatings.
Static-control floors
Conductive and static-dissipative floors contain conductive fillers or fibers, often over a grounded conductive primer and copper grounding strips. Their electrical resistance must remain within the required range throughout the floor’s life, which depends on correct film thickness, grounding and avoiding insulating floor polishes. Resistance is verified after installation and periodically during use.
Walls and ceilings
Walls are commonly coated with high-build epoxy, polyurethane or polyaspartic systems over gypsum board, concrete or block, or are built from prefabricated cleanroom panels. On board, joints must be fully taped and finished first, and fiberglass-reinforced systems may be used for impact resistance in corridors. Ceilings, door frames and pass-throughs are coated with the same system or with compatible finishes so the room envelope is continuous. Masonry block needs pore-filling block fillers before topcoating.
Vaporized or aerosolized hydrogen peroxide decontamination and frequent sporicide use can discolor, soften or embrittle some coatings over time. Ask manufacturers for test data with the facility’s actual disinfectant rotation, concentrations and contact times, or run panel tests before specifying — see chemical resistance testing.
Installation and detailing
- Plan with quality assurance. Define the work as a controlled change, agree on containment, cleaning and requalification, and schedule around production campaigns.
- Test and prepare substrates. Verify concrete moisture and strength, then shot blast or grind; see concrete moisture testing. Prime and fill board and block walls.
- Contain the work. Isolate the area with negative pressure enclosures and dust control so construction dust does not reach operating clean areas.
- Install with full detailing. Form integral coves at floor–wall junctions, seal every penetration, and terminate coatings cleanly at doors, drains and equipment.
- Cure, clean and document. Allow full cure before exposure to disinfectants, then clean, inspect and record products, batches and test results for the validation file.
Ask for a mock-up panel or room section with the actual coves, penetrations and finishes. Quality, validation and maintenance staff can then agree on appearance and cleanability before the full installation begins.
Maintenance and repair
Damaged areas should be repaired promptly with compatible materials and documented like any other change. Cracks at coves, worn traffic lanes and failed sealants around penetrations are typical maintenance items. Cleaning procedures should use products and methods approved by the coating manufacturer, since aggressive scrubbing pads and incompatible chemicals can dull or damage finishes.
Frequently asked questions
Are epoxy floors acceptable in pharmaceutical cleanrooms?
Yes. Seamless epoxy and polyurethane floors are widely used, provided they are coved, resist the disinfectants used and are properly maintained.
Do cleanroom coatings need to be certified?
There is no single certification for cleanroom coatings. Some manufacturers test for particle emission, outgassing or disinfectant resistance, and the facility’s validation process confirms suitability.
Can coating work be done while the plant operates?
Sometimes, in isolated areas with strict containment and pressure control, but most work in classified areas is scheduled during planned shutdowns.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.