Spray Gun Technique
The fundamentals that separate a uniform, in-spec film from sags, dry spray and holidays: distance, angle, speed, overlap, triggering and sequencing.
Key takeaways
- Uniform film build comes from keeping four variables constant: gun distance, gun angle, travel speed and overlap.
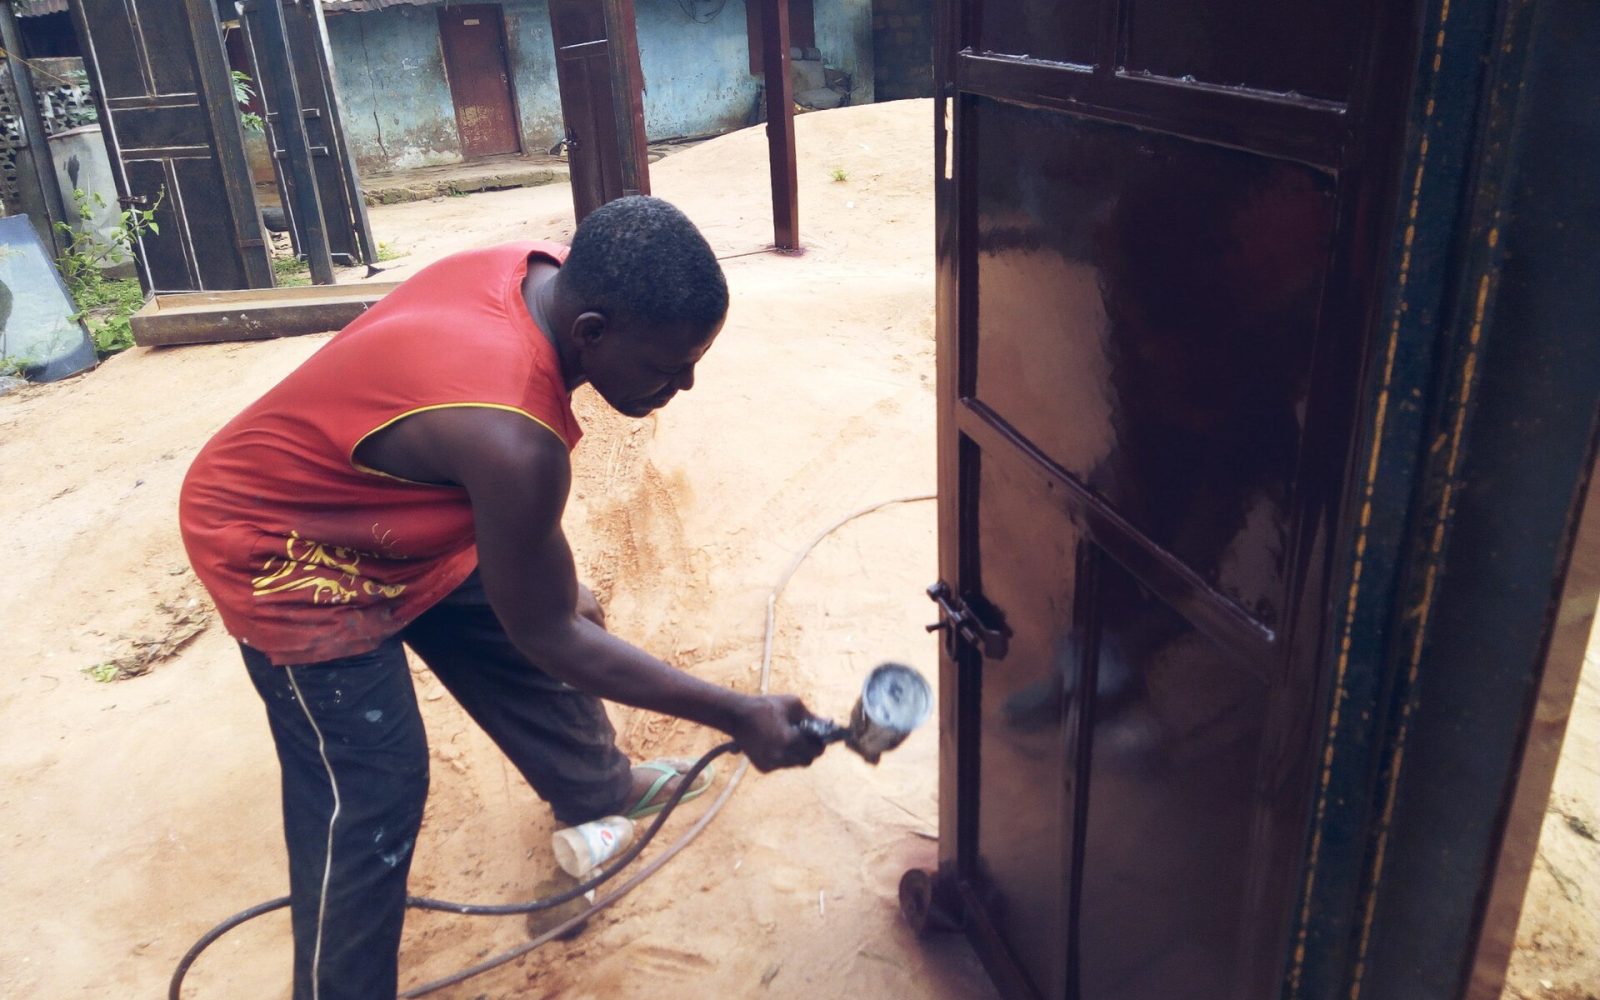
- Hold the gun perpendicular to the surface and move it with the arm and body, not by pivoting the wrist (“arcing”).
- Overlap each pass by about 50% and trigger at the start and end of each stroke so material is not dumped at the ends.
- Coat edges, corners and difficult areas first, then fill in flat areas, and check wet film thickness constantly.
Equipment and materials are only half of a good coating job. The applicator’s hand decides whether the film is uniform, whether edges and corners are covered, and whether the coating reaches its specified thickness without runs. Good spray technique is a learned, repeatable skill built on a few simple rules.
The principles below apply to airless spray, air-assisted airless and HVLP and conventional air spray; the main differences are gun distance and the speed of the pattern.
The four variables
Gun distance
Distance affects film build, pattern width and atomization. Too close and the film builds heavily in a narrow band, inviting sags; too far and droplets dry in flight, producing dry spray and overspray. Airless guns are typically held about 12–18 in (300–450 mm) from the surface; conventional and HVLP guns about 6–10 in (150–250 mm).
Gun angle
Keep the gun perpendicular to the surface in both directions. Tilting the gun up or down makes one edge of the fan heavier than the other, so the overlapping passes no longer blend into an even film.
Travel speed
Move at a steady speed that deposits the target wet film in one pass. Slow strokes overbuild; fast strokes leave thin, starved areas. Speed should be adjusted to the tip and pressure, not the other way around.
Overlap
Each pass should overlap the previous one by about half its width. Aim the center of the fan at the lower edge of the previous pass. Consistent 50% overlap gives an even film because every spot receives two half-coverages.
Arm movement and triggering
The most common beginner error is arcing — swinging the gun from a fixed wrist so it is closer to the surface in the middle of the stroke than at the ends. The result is a heavy band in the center and thin ends. Instead, move the whole arm and shift body weight so the gun travels parallel to the surface. For long runs, walk with the gun rather than reaching.
Triggering prevents buildup at the ends of strokes:
- Start moving. Begin the stroke before pulling the trigger.
- Trigger on. Pull the trigger fully as the gun reaches the edge of the work area.
- Make the pass. Travel at constant speed, distance and angle.
- Trigger off. Release the trigger at the end of the pass while the gun is still moving.
- Index and return. Drop down by half a fan width and make the return pass.
Practice on cardboard or scrap plate and check the result with a wet film gauge at several points across a pass. An even reading across the overlap zone is the quickest proof that distance, angle and overlap are right.
Sequencing the work
Plan the order before triggering. A common sequence for steel structures is:
- Edges, welds and corners first, either as a separate stripe coat or as banding passes, because these areas are hardest to cover and easiest to miss.
- Difficult access next — inside corners, back-to-back angles, the far side of stiffeners and areas behind obstructions.
- Flat areas last, using full, overlapping passes from top to bottom so overspray lands on wet, uncoated or about-to-be-coated areas rather than on finished film.
On large flat surfaces, many applicators make a cross-hatch: one set of passes horizontally, followed immediately by a set vertically. This evens out minor variations and helps eliminate pinholes and holidays.
Inside and outside corners
Spraying straight into an inside corner overbuilds it and can trap air. Instead, spray each face separately, aiming slightly into the corner. Outside corners and edges receive less coating because of fan geometry and surface tension, so band them with a vertical pass aimed directly at the edge.
Pipe and structural shapes
Narrow members are best coated with a narrower fan so material is not wasted past the edges. On pipe, use passes along the length and keep the gun perpendicular to the curvature.
Controlling film thickness
Technique is the applicator’s main control over dry film thickness. Frequent wet film thickness readings during application allow immediate correction, while dry readings are confirmed later by the inspector. Both thin spots and overbuild are defects: thin film reduces barrier protection, while excessive film can crack, sag or trap solvent.
If film build is consistently off target, change one variable at a time. Adjust gun speed first; if the needed speed becomes impractical, change the tip size or fan width rather than distorting distance or pressure. See airless spray tip selection.
Troubleshooting technique-related defects
| Defect | Likely technique cause | Correction |
|---|---|---|
| Sags and runs | Gun too close, too slow, too much overlap | Increase distance or speed; check wet film |
| Dry spray | Gun too far, angled, or air too hot and windy | Move closer, keep perpendicular, shield from wind |
| Striping (bands) | Inconsistent overlap, worn tip, low pressure | Hold 50% overlap; replace tip; raise pressure |
| Heavy ends of passes | Late trigger release, arcing | Trigger on the move; keep gun parallel |
| Orange peel | Poor atomization, too far, too thin | Adjust pressure, distance and film build |
| Thin edges and holidays | No banding or striping | Stripe or band edges first |
Environmental conditions also matter: wind can carry atomized coating away from the surface, and high temperatures accelerate solvent loss in flight. Shielding the work or adjusting the timing of application can be as important as the applicator’s hand.
Frequently asked questions
Why is 50% overlap recommended?
The spray fan delivers less coating at its edges than at its center. Overlapping by half the fan width blends the lighter edges so that the total film is even across the surface.
Should I spray one heavy pass or several lighter passes?
Follow the product data sheet. Many high-build coatings are designed for a single multi-pass coat applied wet-on-wet, but each pass should be even and within the coating’s sag resistance.
Is it acceptable to wave the gun to blend areas?
Flicking or arcing the gun produces uneven film. Blend by overlapping controlled passes, and use a cross-hatch on large areas.
How can I tell if my technique is consistent?
Take wet film readings across several passes and at the start, middle and end of strokes. Consistent readings indicate stable distance, angle, speed and overlap.
Educational reference. Coating performance varies by formulation. Always follow the manufacturer’s product data sheet, safety data sheet and your project specification.